2 subprograms – HEIDENHAIN TNC 410 User Manual
Page 207
9 Programming: Subprograms and Program Section Repeats
194
9.1 Mar
king Subpr
ogr
ams and Pr
ogr
am Section Repeats;
9.2 Subprograms
9.1 Marking Subprograms and
Program Section Repeats
Subprograms and program section repeats enable you to program a
machining sequence once and then run it as often as desired.
Labels
The beginnings of subprograms and program section repeats are
marked in a part program by labels.
A label is identified by a number between 1 and 254. Each label can
be set only once with LABEL SET in a program.
LABEL 0 (LBL 0) is used exclusively to mark the end of a
subprogram and can therefore be used as often as desired.
9.2 Subprograms
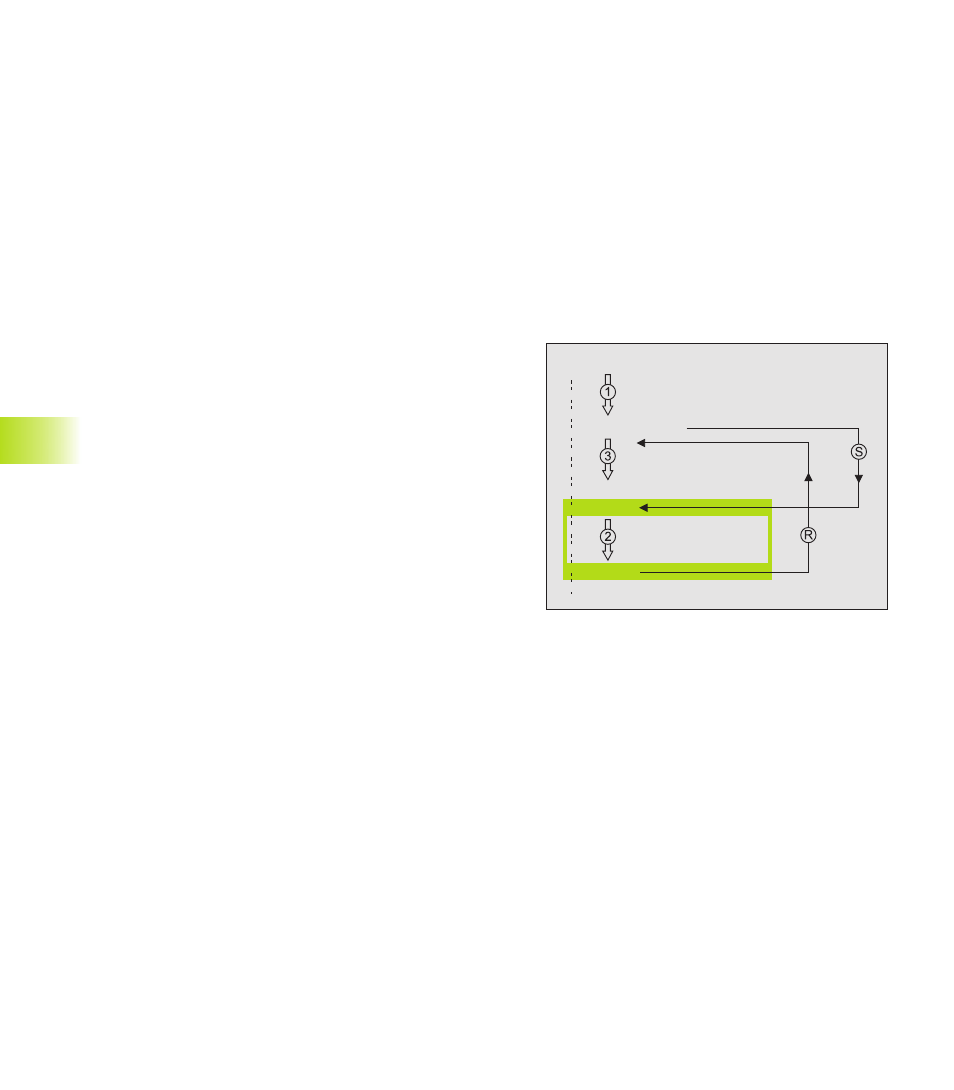
Operating sequence
1 The TNC executes the part program up to the block in which a
subprogram is called with CALL LBL.
2 The subprogram is then executed from beginning to end. The
subprogram end is marked with LBL 0.
3 The TNC then resumes the part program from the block after the
subprogram call.
Operating constraints
■
A main program can contain up to 254 subprograms.
■
You can call subprograms in any sequence and as often as
desired.
■
A subprogram cannot call itself.
■
Write subprograms at the end of the main program (behind the
block with M2 or M30).
■
If subprograms are located before the block with M02 or M30,
they will be executed at least once even if they are not called.
BEGIN PGM ..
CALL LBL1
L Z+100 M2
LBL1
LBL0
END PGM ...