3 pr ogr am run – HEIDENHAIN TNC 410 User Manual
Page 254
241
HEIDENHAIN TNC 410
1
1
.3 Pr
ogr
am Run
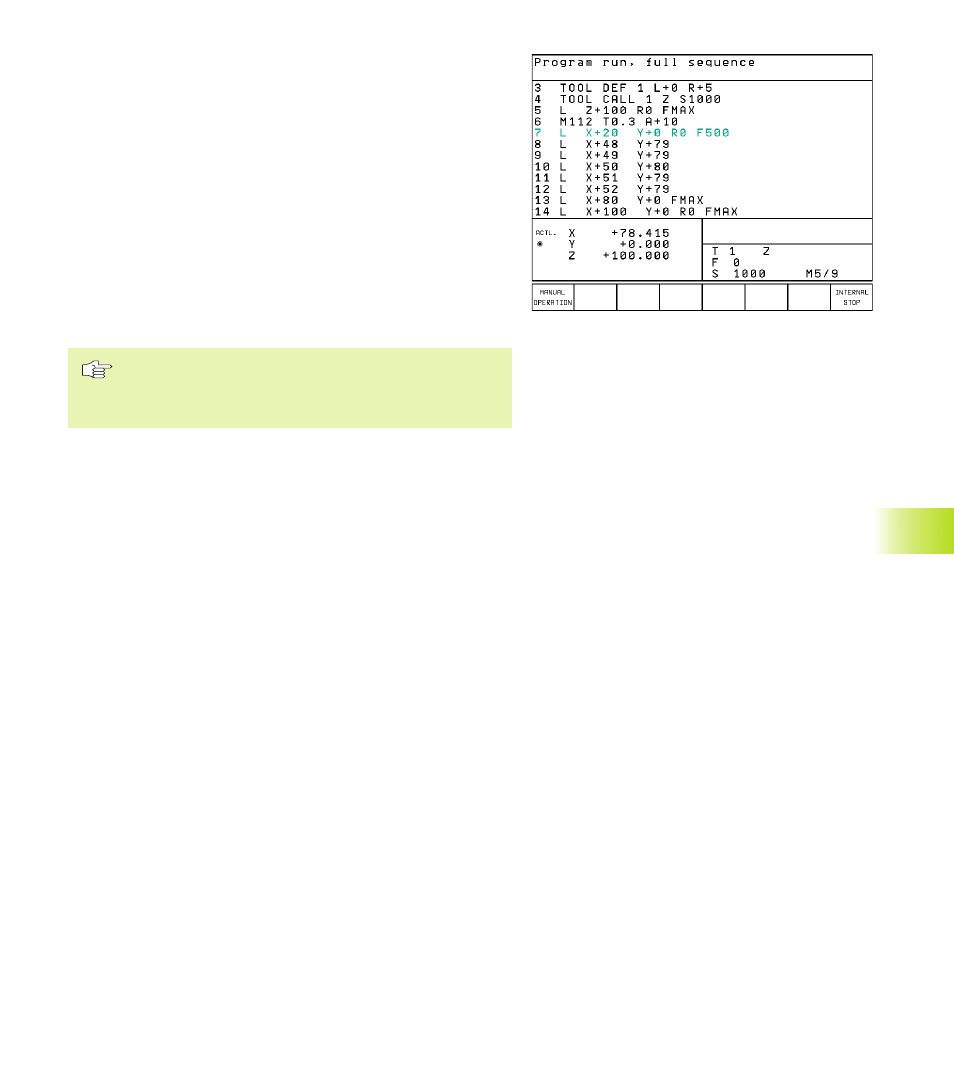
Moving the machine axes during an interruption
You can move the machine axes during an interruption in the same
way as in the Manual Operation mode.
Example:
Retracting the spindle after tool breakage
ú
Interrupt machining.
ú
Enable the external direction keys: Press the MANUAL OPERATI-
ON soft key.
ú
Move the axes with the machine axis direction buttons.
Use the function „Returning to the Contour“ (see below) to return
to a contour at the point of interruption.
Resuming program run after an interruption
If you interrupt a program run during a fixed cycle, you
must resume the program from the beginning of the
cycle. This means that some machining operations will
be repeated.
When a program run is interrupted, the TNC stores:
■
The data of the last defined tool
■
Active coordinate transformations
■
The coordinates of the circle center that was last defined
■
The current count of program section repeats
■
The number of the block where a subprogram
or a program section repeat was last called