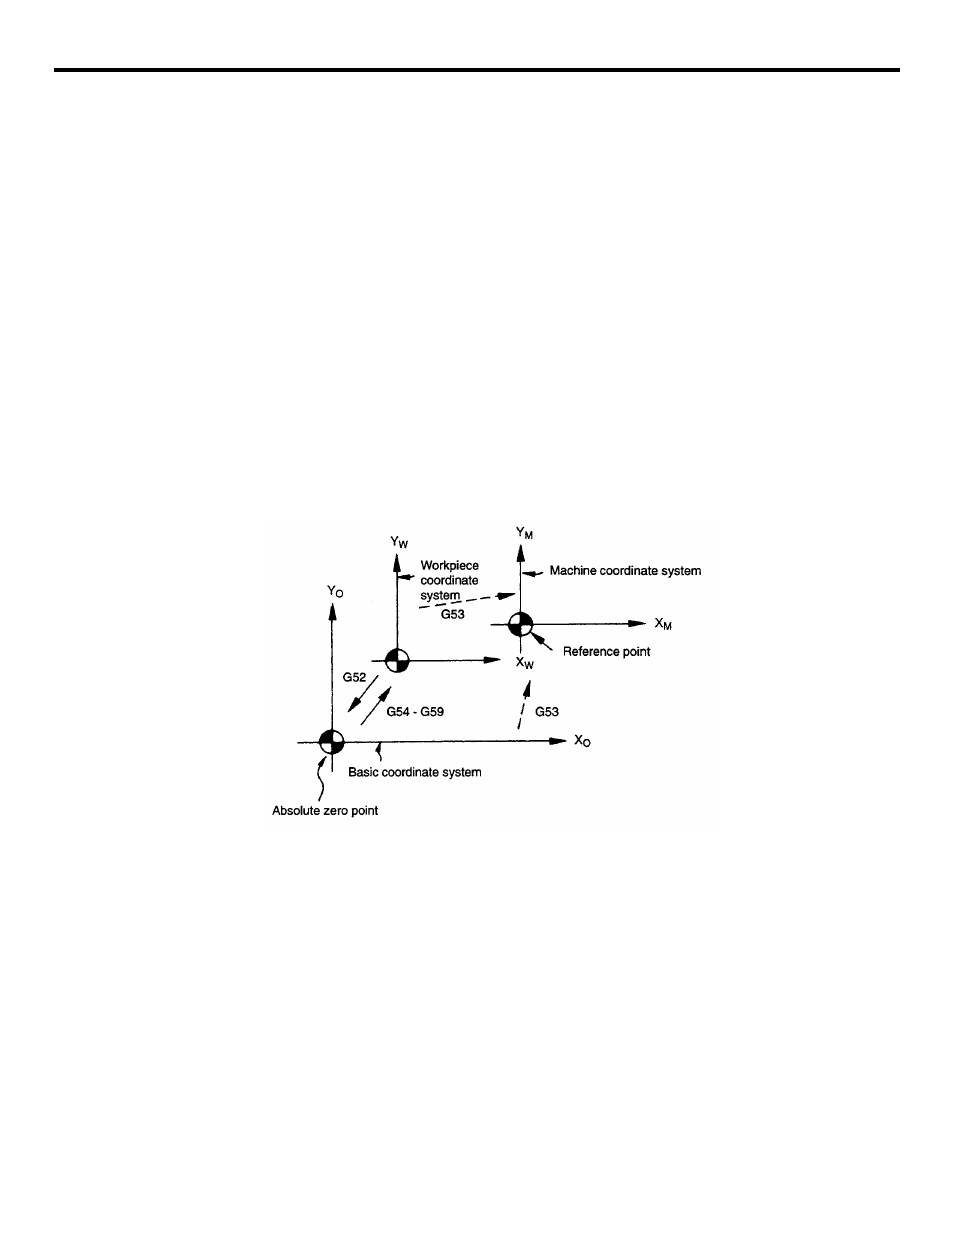
5 machine coordinate system (g53), Figure 3.1.5.1: machine coordinate system – Yaskawa YASNAC PC NC Programming Manual User Manual
Page 63
3 - 13
YASNAC PCNC Programming Manual
Chapter 3: Movement Control Commands
(2) Supplements to Local Coordinate System Setting Commands
•
In the state where a workpiece coordinate system and local coordinate system have
been set, G92 command must not be executed. An operation to set a coordinate sys-
tem at the NC operation panel must also be avoided. Also refer to supplements indi-
cated in “Base Coordinate System (G92)”.
•
If G52 is executed while this optional function is not selected, it cancels the workpiece
coordinate system (G54 to G59).
•
The local coordinate system is canceled by the reset operation.
3.1.5
Machine Coordinate System (G53)
The machine coordinate system, specific to the machine, is determined by the execution of refer-
ence point return operation. It has the origin (0, 0, 0) at the reference point.
(1) Command Format
By specifying “(G90) G53 X • • • Y • • • Z • • •;”, axis move commands in this are executed in
the machine coordinate system. G53 is a non-modal G code.
FIGURE 3.1.5.1: Machine Coordinate System